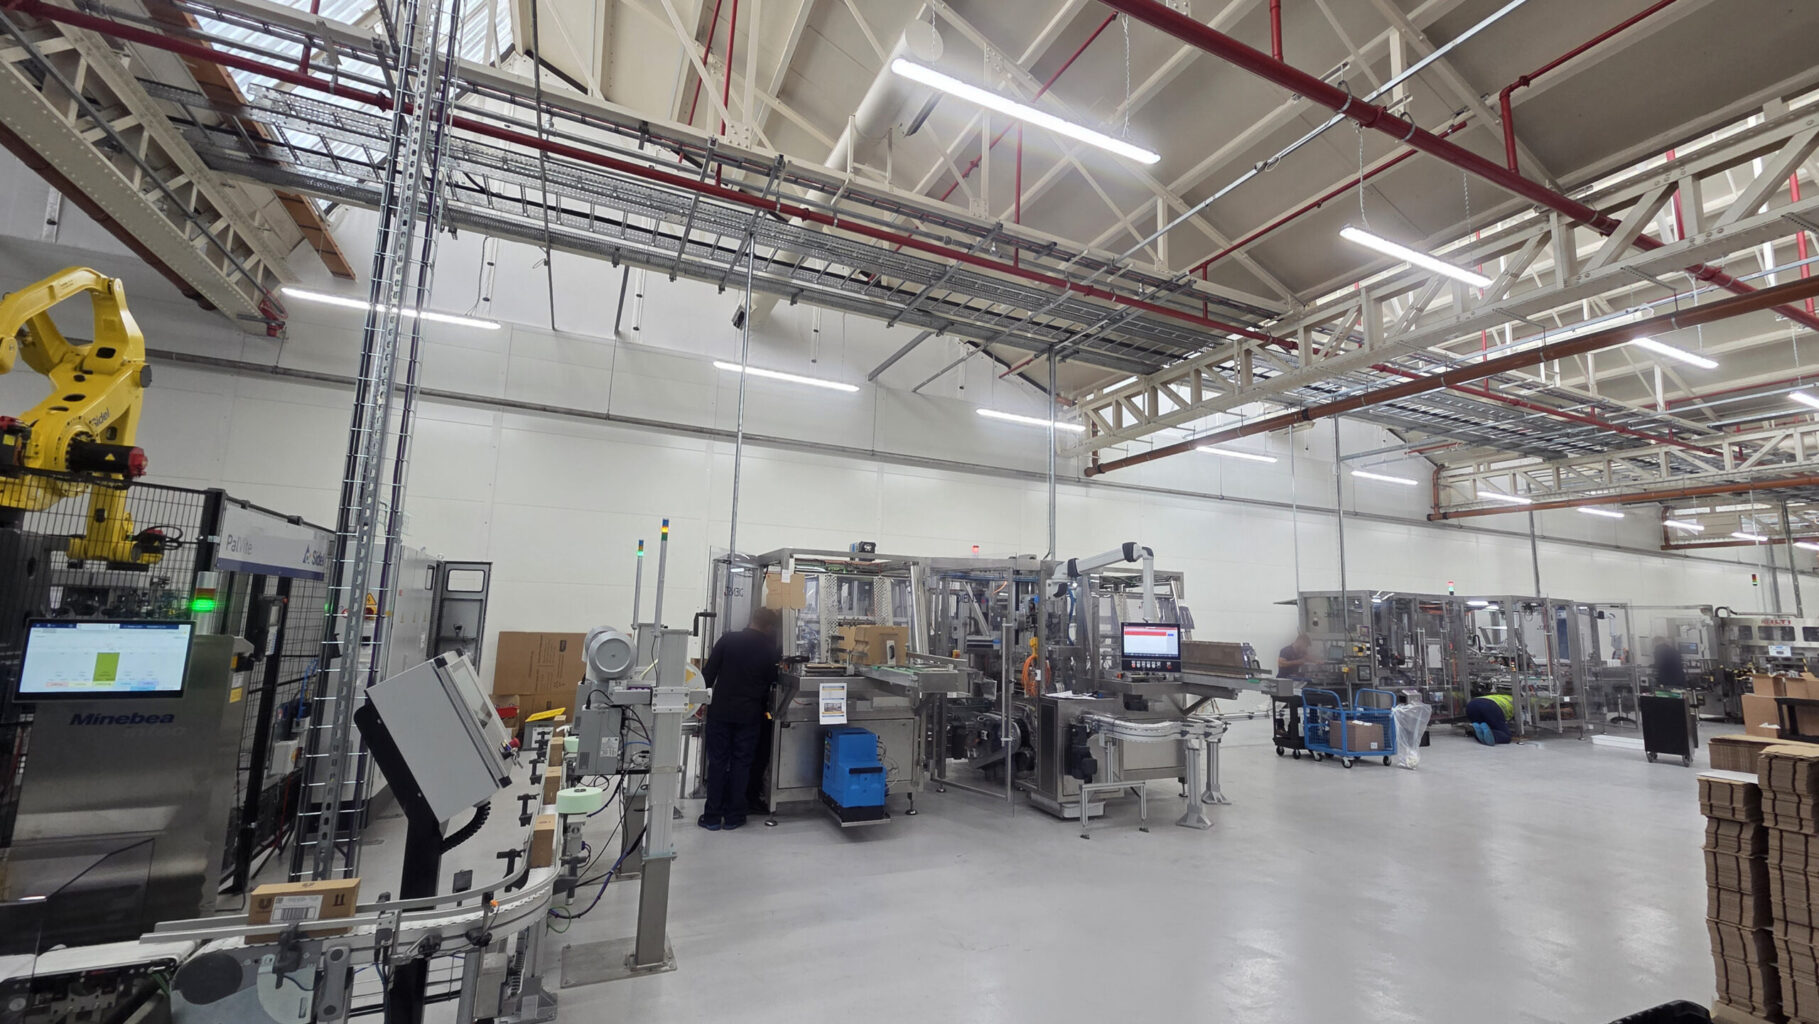
Fabric partition wall provides 99% dust protection
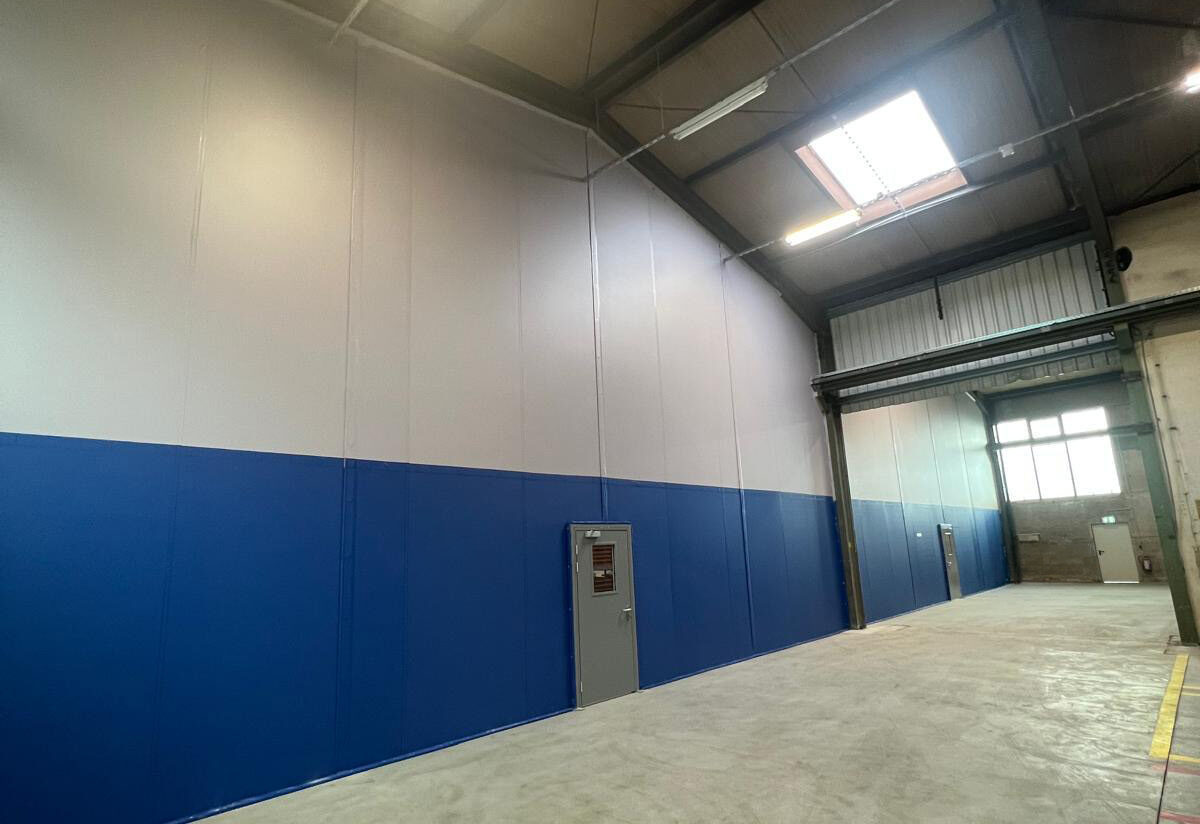
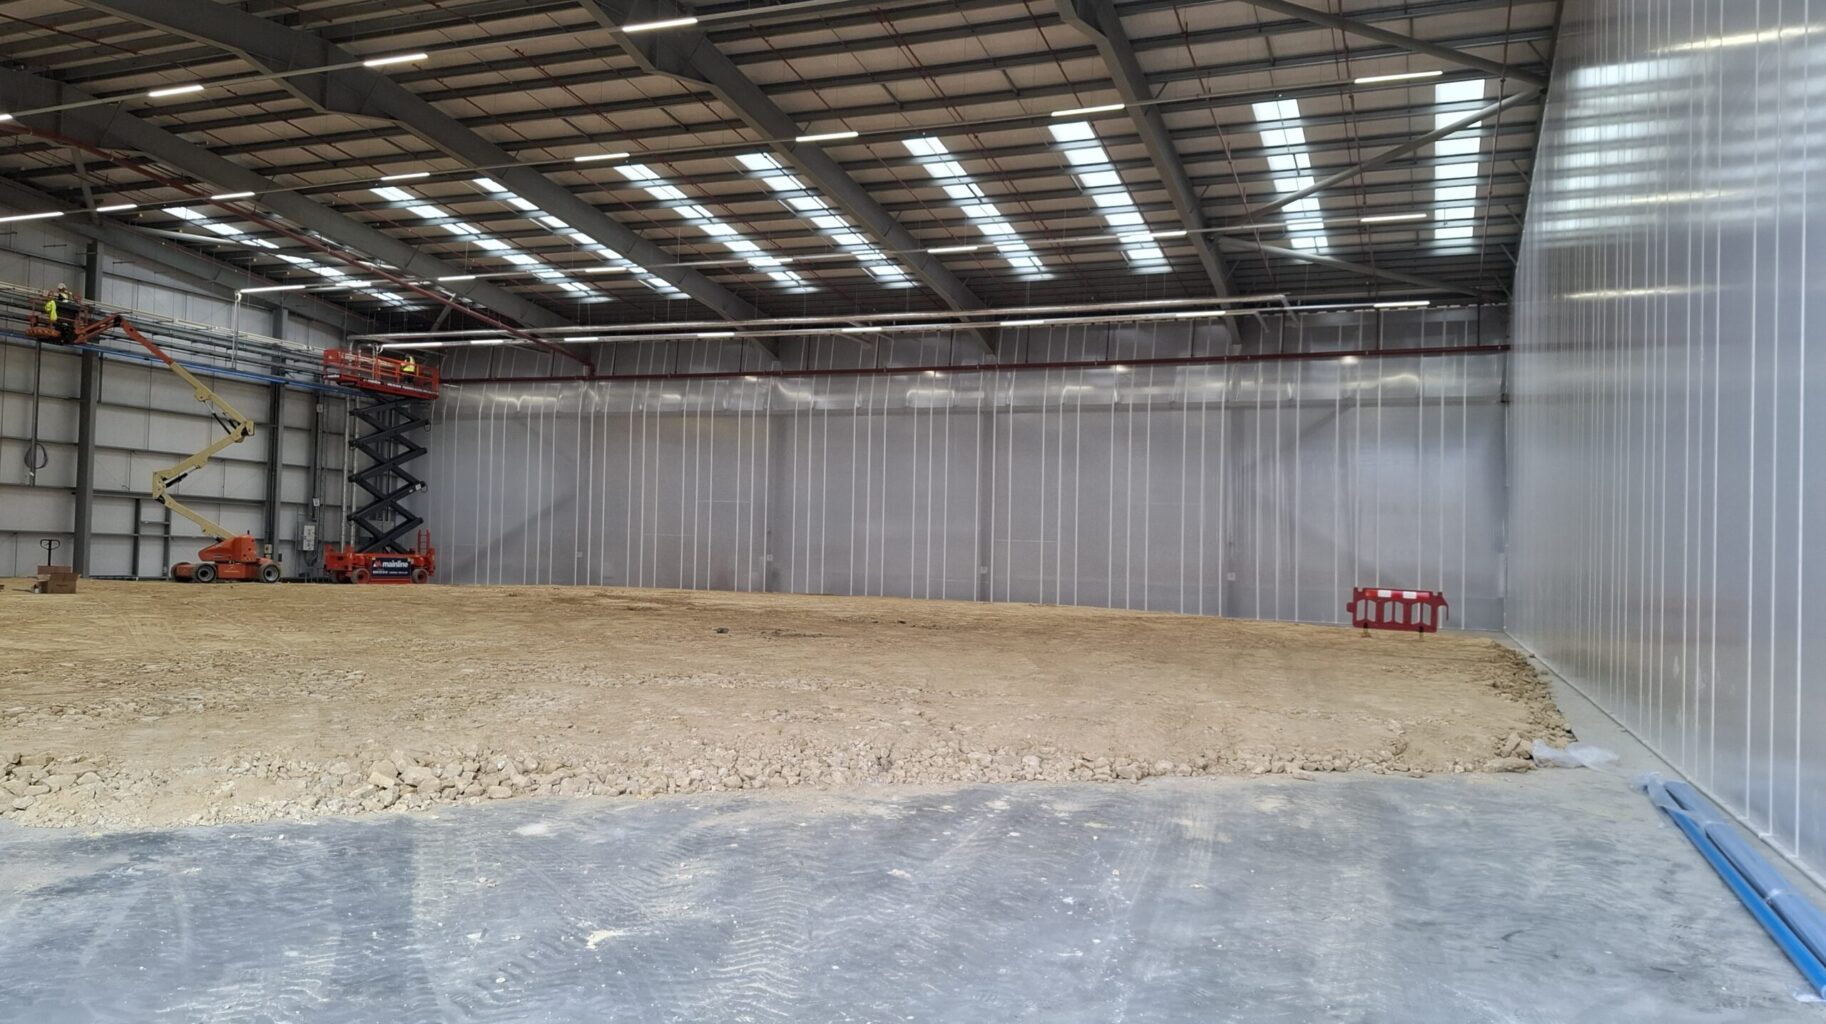
Westgate Global recommended using Flexiwall®, a tensioned fabric partition wall, to create two clearly defined functional areas within the warehouse. Installed floor-to-ceiling, Flexiwall provides an over 99% dust-tight seal, using a unique V-overlap panel connection and high-tensile cables to prevent dust, debris, and cross-contamination.
By dividing the warehouse into two areas, the Flexiwall system minimised the risk of dust spreading between zones. In a brewing environment, airborne particulates can quickly cause issues and unplanned downtime: settling open bottles, crates, or packaging; or affecting nearby equipment, from sensors on bottling lines to conveyor mechanisms. Physically separating the two process areas addressed this risk, helping to protect both product quality and logistics operations.
Following a site survey, the team designed and manufactured the Flexiwall components to match the warehouse’s exact measurements. Because the system requires no additional steelwork and causes no damage to the structure or floor, installation could be carried out in close proximity to ongoing operations, with minimal impact on production schedules. The flexible panels were suspended from the ceiling, tensioned, and securely anchored to the floor, taking up just 50mm of floor space and keeping installation quick and clean while maximising usable floor area around racking and equipment.
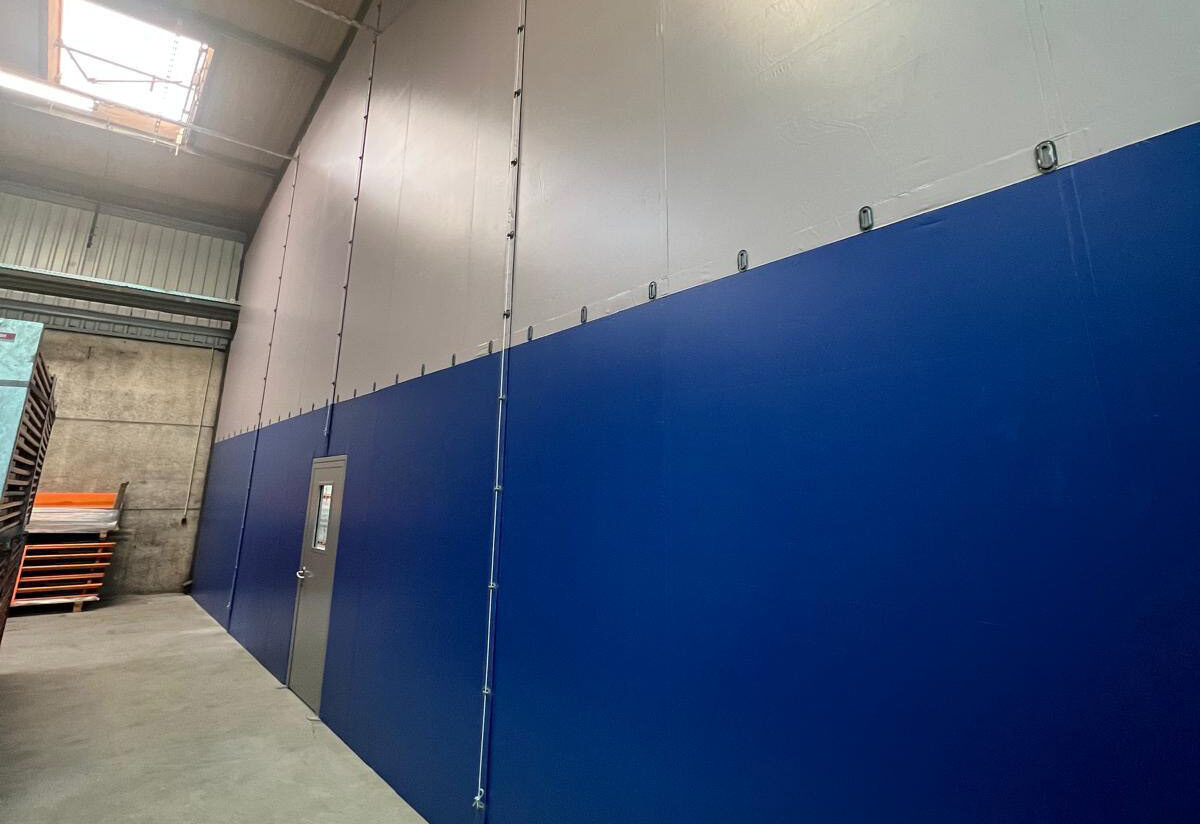
Westgate Global installed two runs of Flexiwall, each 14 metres long and 7.7 metres high. The flexible nature of the solution means it can be fitted around existing infrastructure, including warehouse equipment, conveyor lines, pipes, and ducts. Staff doors were installed, allowing Brewery employees to move between zones without compromising the partition’s effectiveness.
Designed with evolving spaces in mind, the robust, reusable nature of the Flexiwall fabric means that, should the warehouse be redesigned in future, the system can be easily adapted, dismantled, or relocated.
Westgate Global handled the project end-to-end. The team worked closely with the client to define requirements, designing and manufacturing components to fit the warehouse’s exact dimensions, and carrying out the installation around live operations. The solution enabled the brewery to successfully improve efficiency and create a controlled environment for its future needs.